
1. Industry Overview
Against the backdrop of full‑scale implementation of the new‑type power system and continuous upgrading of urban‑rural distribution networks, end‑user scenarios such as new‑energy power stations, industrial & commercial power distribution projects, rail transit and municipal power‑supply engineering keep expanding, driving steady growth in market capacity demand for medium‑voltage ring main units (RMU) and complete switchgears. As core mainstay equipment for power distribution systems, ring main units and switchgears involve complicated manufacturing procedures and strict assembly‑precision requirements, with high standards for production premises, material‑handling processes and assembly specifications. At present, most domestic electrical equipment manufacturers still adopt the traditional fixed‑station production mode, without dedicated switchgear production lines and ring‑main‑unit assembly lines, resulting in low overall production automation.
Traditional production relies on overhead cranes and forklifts for manual cabinet transfer, without standardized workflows for switchgear assembly lines. Cabinet handling, positioning and tilting are all labour‑intensive, leading to low productivity and high labour costs. Heavy‑weight cabinets are prone to sheet‑metal deformation, paint chipping and cabinet misalignment during frequent transfers, which directly compromise subsequent assembly and factory‑outlet quality. Furthermore, fixed‑station operations cannot satisfy multi‑sided cabinet assembly requirements. When technicians perform wiring and component installation on the rear and side surfaces of cabinets, they frequently bend, stoop or work at height. Poor assembly consistency, non‑standard wiring workmanship and chaotic cross‑processes are common pain points in electrical‑equipment manufacturing.
To fully address the drawbacks of conventional manual production, standardized switchgear production lines and ring‑main‑unit assembly lines have become core facilities for electrical manufacturers’ intelligent transformation. This intelligent assembly line for ring main units and switchgears adopts an RGV rail‑guided transport system as the key logistics carrier. It integrates hardware modules including cabinet tilting fixtures, automatic station transfer, centralized electric control, safety protection and high‑voltage testing. It realizes full‑process inline operations for switchgears and ring main units: cabinet feeding, pre‑assembly, component fitting, busbar connection, secondary wiring, commissioning & testing and finished‑product offloading. Standardized operations on dedicated switchgear production lines and ring‑main‑unit assembly lines effectively standardize production workflows, stabilize product quality, shorten manufacturing cycles and reduce labour dependency, catering to large‑scale, standardized and mass‑production requirements for complete electrical equipment.
2. General Description of RGV‑based Assembly Line for Ring Main Units & Switchgears
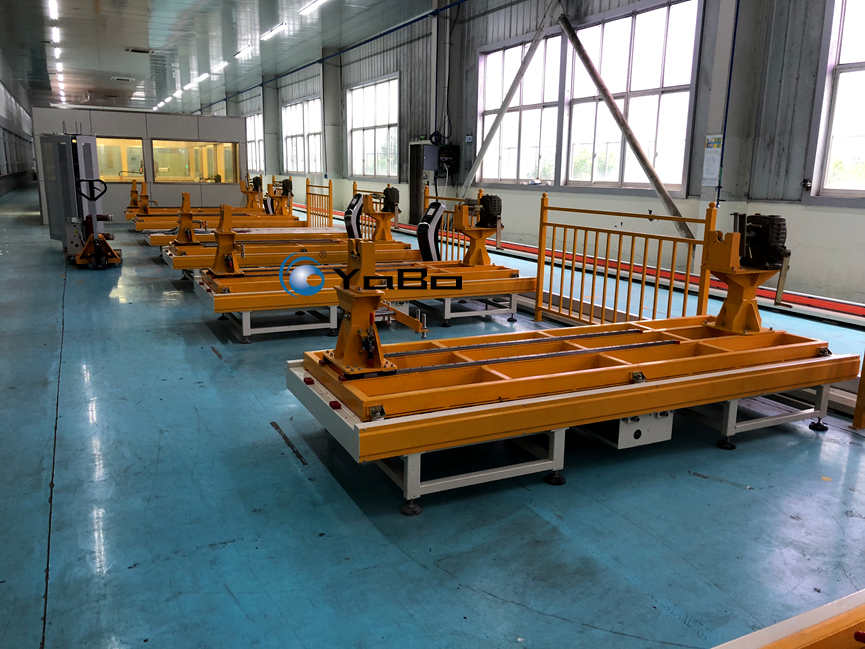
This complete set of switchgear production line and ring‑main‑unit assembly line is a closed‑loop circulating station‑based assembly system. Featuring proven, stable and highly‑adaptable construction, it is fully suitable for mass assembly of medium‑voltage switchgears and ring main units. The whole line consists of six major modules: cabinet tilting fixture stations, RGV rail transport system, equipment safety‑protection system, high‑voltage withstand‑test compartment, auxiliary handling equipment and centralized electrical control system. Designed for standard steel‑structure industrial workshops with epoxy‑resin flooring, it meets the requirements for dust‑free, tidy and safe production environments for electrical complete‑set equipment.
Tilting fixture stations serve as the core bearing units for ring‑main‑unit assembly lines and switchgear assembly lines. Fabricated from thickened section steel by welding, they feature high structural rigidity, heavy load‑bearing capacity and anti‑deformation performance for long‑term stable support of complete cabinets during assembly. Each fixture station corresponds to one independent production station. Dedicated mechanical tilting heads fitted at both ends incorporate geared motors, self‑locking clamping mechanisms and transmission assemblies. Positioning slide rails and quick‑release clamps are mounted on the worktop. After the cabinet is lifted into position, clamps fasten it securely to prevent positional shift, and the tilting mechanism performs stable 90‑degree cabinet rotation. With the tilting function, operators can install components, fit busbars and complete secondary wiring on cabinet sides and rear surfaces from the front side, without stooping or working at height. It greatly lowers assembly error rates, unifies assembly specifications and improves throughput and workmanship across the whole switchgear production line. Adjustable support feet at the bottom provide stable support for offline maintenance and station positioning, preserving equipment operating accuracy.
The RGV rail‑guided transport system constitutes the automatic logistics core for switchgear production lines and ring‑main‑unit assembly lines. Special industrial rails are laid on the workshop floor for rail‑mounted RGV shuttles to automate transfer of fixtures and cabinets. Abolishing manual handling by forklifts and overhead cranes, the whole system runs under automatic dispatching. During production, RGV shuttles convey fixture stations loaded with cabinets sequentially to feeding station, pre‑assembly station, component‑fitting station, wiring station, commissioning station and testing station to complete all manufacturing steps in sequence. Upon assembly completion, RGV automatically transports cabinets to the high‑voltage test zone. After passing tests, cabinets are moved to the finished‑product offloading station, while empty fixtures circulate back to the feeding end for closed‑loop cyclic production. Automatic RGV transfer precisely controls production takt time, avoids process bottlenecks and station disorder, and eliminates cabinet collision, deformation and misalignment caused by manual handling, substantially boosting operational stability of the ring‑main‑unit assembly line.
A full‑range standardized safety‑protection system is implemented along the assembly line. Steel safety railings around stations strictly separate operator working zones from equipment movement zones to stop personnel from entering RGV travelling areas and ensure on‑site safety. A standalone enclosed high‑voltage withstand‑test room with observation windows is installed at the line end. High‑voltage withstand tests, insulation checks and electrical‑performance evaluations are incorporated inline, enabling integrated assembly & testing without cross‑workshop transfers and streamlining production workflows. Manual hydraulic handling equipment is deployed for short‑distance transfer of small‑size materials, auxiliary parts and fixture accessories to support auxiliary line‑side operations. The complete switchgear production line is equipped with a centralized electrical‑control system for unified management of RGV dispatching, fixture tilting, station signal interaction and equipment interlock start‑stop. It supports connection with the workshop MES (Manufacturing Execution System) to collect real‑time data including station status, process progress and equipment performance for intelligent production management.
3. Customizable Solutions & Main Technical Specifications
This ring‑main‑unit assembly line and switchgear production line support full‑scenario customized engineering. Tailored solutions can be delivered according to manufacturers’ product specifications, capacity requirements, workshop dimensions and production layouts, covering both small‑to‑medium‑scale flexible production and large‑volume standardized mass‑manufacturing.
- Customized Fixture Load‑bearing: Fixture load capacity can be customized from 1.5 t to 4 t for assembling ring main units and switchgears of varying dimensions and weights. Tilting angle is adjustable within 0‑90°, with controllable uniform tilting speed and smooth shock‑free start‑stop. Worktop dimensions are customized to match the maximum cabinet outer dimensions of the customer. Clamping structures can be specially reworked for different cabinet designs to realize multi‑model mixed‑line production.
- Customized Line‑station Layout: The number of stations on the switchgear assembly line can be flexibly configured, typically ranging from 6 to 16 standard stations, including feeding station, pre‑assembly station, component‑fitting station, busbar‑mounting station, secondary‑wiring station, tilting‑operation station, mechanical‑commissioning station, high‑voltage test station and finished‑product offloading station. Station quantity can be increased or decreased as required. Line layouts are available in straight‑line and closed‑loop rectangular configurations to adapt to workshops of different length‑width ratios and maximize floor‑space utilization.
- Customized RGV System: RGV shuttles offer two power‑supply options: battery power supply and conductor‑rail power supply to suit different workshop power‑distribution conditions. Payload and travelling speed are matched to site requirements, with adjustable speed ranging from 0‑20 m/min. Built‑in features include high‑precision positioning, automatic anti‑collision, fault alarm and emergency stop for stable and safe operation. Both manual operation and fully‑automatic cyclic modes are supported. A multi‑vehicle dispatching system enables station call‑up, automatic waiting and self‑diagnosis to guarantee continuous stable operation of the ring‑main‑unit assembly line.
- Optional Functional Modules: Dimensions and configurations of the high‑voltage test room can be customized on request. Optional items include station lighting, station power outlets and material pallets to improve working conditions. MES data‑interface expansion is available for production‑data upload, process traceability and output statistics. Safety light curtains, acoustic‑optical alarms and zone‑protection interlocks can be added to raise equipment safety levels, fully accommodating manufacturers’ production‑upgrade demands.
Basic Reference Technical Parameters
Applicable Products: Medium‑voltage ring main units, complete‑set switchgears Fixture Tilting Angle: 0‑90° adjustable RGV Positioning Accuracy: ±2 mm Operating Environment: Workshop temperature 0‑45 °C, industrial workshop with standard epoxy‑resin flooring Control Mode: Local manual operation + full‑line automatic cyclic operation
The customized switchgear production line and ring‑main‑unit assembly line feature rational layout, stable performance and strong adaptability. They effectively help electrical‑equipment manufacturers optimize production workflows, raise assembly standardization, cut labour costs and stabilize product quality. They represent key capital equipment for intelligent upgrading and capacity expansion among power‑distribution‑equipment manufacturers.